
Steel Structure Quality Verification Before Project Delivery
Learn steel structure quality checks, inspection steps, documentation, and pre-delivery verification.
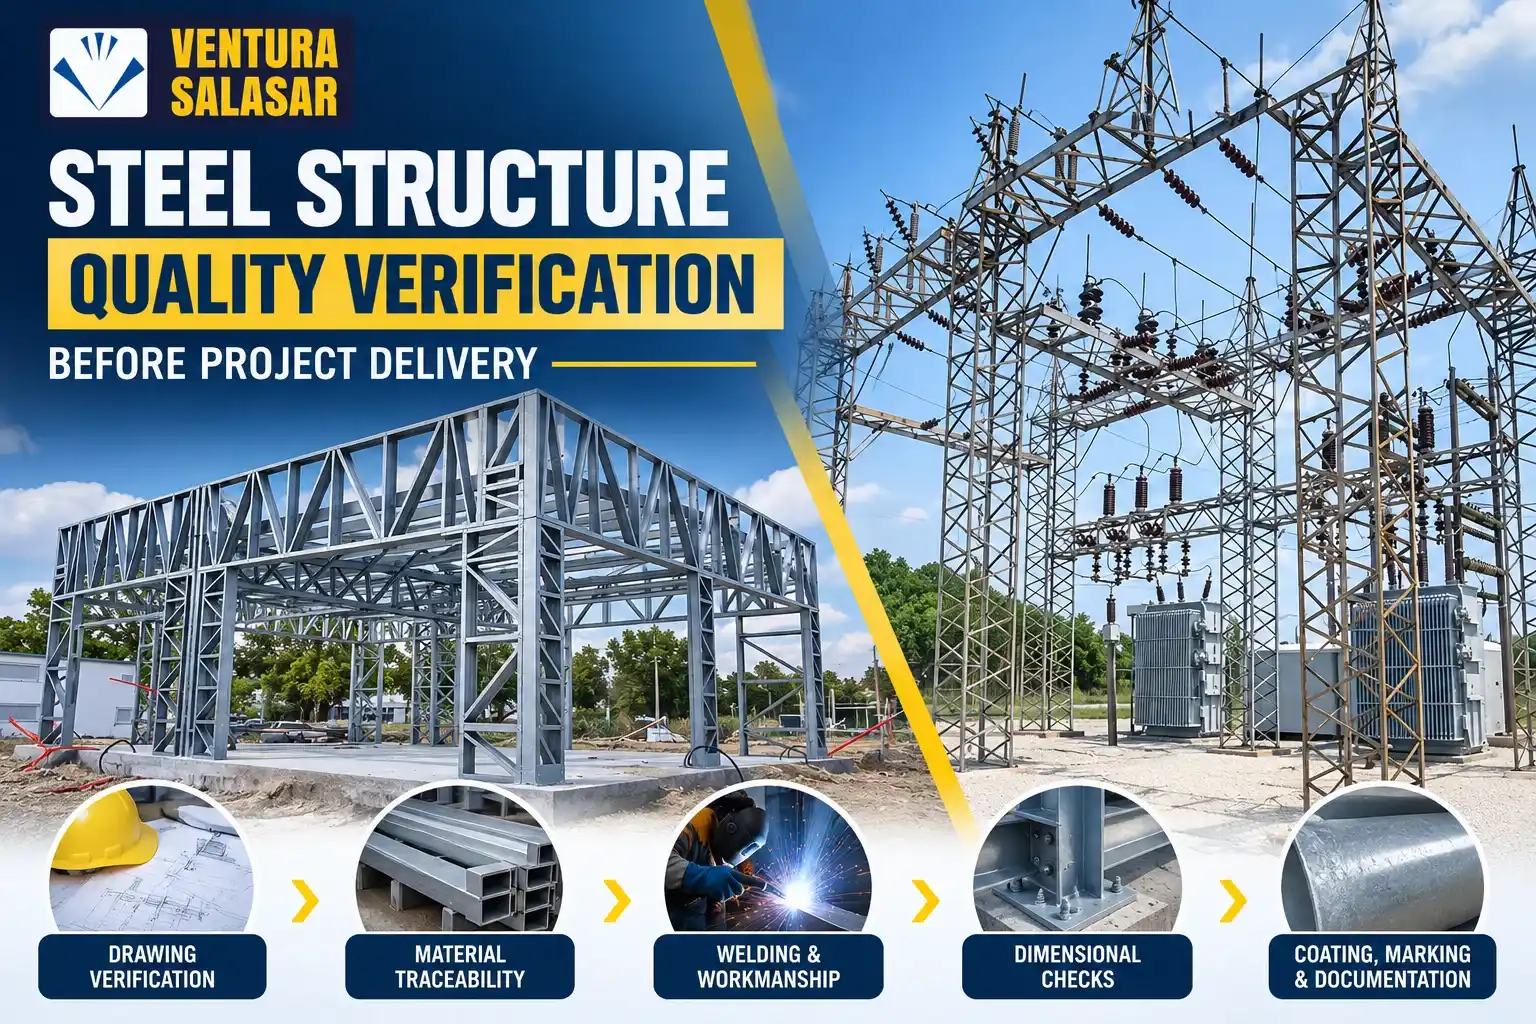
Steel structure quality verification before delivery should confirm five things: the fabricated items match approved drawings; materials are traceable; welding and workmanship meet the project acceptance criteria; dimensions and trial interfaces are correct; and coatings, markings, documents and packing are ready for site installation. A final visual check alone cannot prove these requirements. Verification must follow an approved inspection and test plan from material receipt through dispatch.
The project team should define hold points, records and acceptance criteria before fabrication begins. Ventura Salasar presents fabricated structures, heavy steel structures and related services online. For a specific order, the purchase specification, approved drawings and quality plan remain the governing references.
Why Pre-Delivery Inspection Matters
A mismatch that is easy to correct in the workshop can become costly at site. Incorrect hole centres, reversed plates, missing cleats, excess distortion or damaged coating may stop erection, require unsafe field modification or delay other contractors. Pre-delivery verification reduces this risk by finding nonconformities while suitable people, tools and controlled processes are still available.
Inspection also creates evidence. Marked drawings, material certificates, weld records, dimensional reports, coating measurements and release notes help the site team identify members and understand what was accepted. They do not replace competent erection checks, but they establish a trustworthy handover baseline.
Build the Inspection Plan Before Fabrication
| Stage | Typical control | Record |
|---|---|---|
| Document review | Approved drawings, specification and ITP | Review register |
| Material receipt | Grade, size, condition and traceability | MTC and receipt report |
| Fit-up | Joint preparation, orientation and dimensions | Fit-up checklist |
| Welding | Procedure, welder status and inspection | Weld map and reports |
| Coating | Preparation, thickness and repair | Coating report |
| Final release | Dimensions, marking, packing and dossier | Dispatch release note |
The inspection and test plan should state each operation, acceptance reference, responsibility, sampling, record and notification requirement. Hold points stop work until approval; witness points give the buyer an opportunity to attend; review points require document acceptance. These terms should be agreed, not assumed.
Create a fabrication data book index at the start. If records are collected only at the end, missing traceability or inspection signatures may be impossible to reconstruct. Assign unique drawing, member, weld and report identifiers that can be reconciled.
1. Verify Approved Drawings and Revision Control
Fabrication should use released drawings with a clear revision and status. Confirm that connection details, member sizes, material grades, hole patterns, weld symbols, camber, tolerances, coating system and piece marks are consistent across general arrangement, shop drawings and bills of material. Superseded copies should be removed from workstations.
Record requests for information and approved changes. A verbal site preference should not be introduced into production without design authorization. Ventura offers steel detailing and structural designing; the project must still identify the engineer responsible for design approval and change control.
Interface dimensions deserve special attention
Foundation bolt centres, base-plate holes, splice geometry, equipment interfaces and connections to existing structures can govern installation. Verify them against coordinated information, not one isolated drawing. Where practical, use templates, jigs or trial assembly to confirm repeatability.
2. Confirm Material Identity and Traceability
Check material type, grade, dimensions and condition against the bill of material and purchase documents. Review mill or manufacturer certificates where required and link heat or batch identification to cut parts through the agreed traceability method. Substitution of grade or section requires formal approval.
Inspect plates and sections for lamination indications, heavy corrosion, damage, twist or other conditions that could affect fabrication. Storage should prevent contamination and uncontrolled mixing. Consumables such as welding electrodes, wire, gases, fasteners and coating materials also need correct identification, shelf life and storage.
3. Inspect Cutting, Holes and Edge Preparation
Verify part dimensions, squareness, cut quality, notches, copes, holes and bevels before assembly hides access. Remove detrimental burrs and slag. Hole diameter, pitch, edge distance and alignment should match approved details. Unauthorised thermal enlargement of holes is a serious warning sign.
Check that piece marks remain readable and traceable after cutting. For repeated components, first-off inspection can confirm the machine setup before the batch proceeds. Measuring equipment must be suitable, identifiable and within calibration requirements.
4. Control Fit-Up Before Welding
| Fit-up check | What to verify |
|---|---|
| Member orientation | Top, bottom, handedness and connection direction |
| Joint geometry | Root gap, bevel, alignment and contact surfaces |
| Attachment location | Cleats, stiffeners, lugs and temporary items |
| Restraint and sequence | Method limits shrinkage and distortion |
| Cleanliness | Joint area is free from moisture and contaminants |
| Tack welding | Approved personnel, consumables and sound tacks |
Fit-up inspection prevents wrong parts or geometry from being permanently welded. Measure key diagonals, offsets, levels and assembly dimensions before release. Temporary attachments should be controlled because careless removal can damage the base metal.
5. Verify Welding Quality
Welding should follow approved procedures applicable to the material, joint, thickness, process and position. Confirm welder or operator qualifications, consumable control, preheat and interpass requirements, sequence and environmental protection. The inspector should use weld maps or another method to link joints with inspection records.
Visual inspection examines weld size, length, profile, continuity, termination, undercut, overlap, cracks, porosity indications, arc strikes and surrounding damage. Required nondestructive examination should be performed by qualified personnel using approved procedures. The applicable project code and specification determine methods, extent and acceptance—not a generic percentage copied from another project.
Repairs must be controlled
A rejected weld should be identified, evaluated, removed and repaired through an approved method, then reinspected. Repeated repairs or recurring defect types require root-cause action. Grinding a visible indication without documenting the disposition is not an acceptable quality process.
6. Check Dimensions and Assembly Geometry
Final dimensional inspection should cover member length, straightness, sweep, camber, flange and web alignment, plate position, hole pattern, splice faces, base-plate flatness and overall assembly geometry. Use the tolerances stated in the contract and applicable fabrication standard.
Record actual values for critical dimensions rather than only ticking “OK.” Trial assembly is valuable for complex nodes, repeated modular sections or interfaces with limited site adjustment. Photographs can supplement, but not replace, a signed dimensional report.
7. Verify Bolts and Connection Components
Confirm bolt assemblies, nuts and washers match the approved grade, size, finish and system. Store them to prevent corrosion, contamination and mixing. The dispatch list should allocate connection hardware by erection sequence or member package. If preloaded connections are required, installation and verification procedures must be defined for site execution.
Check that faying surfaces, holes and access suit the connection design. Do not apply incompatible paint to surfaces that must meet a specified slip condition. Loose items such as shims, splice plates and templates should carry durable identification.
8. Inspect Surface Preparation and Galvanizing or Paint
Surface preparation and coating quality depend on the specified system. For paint, confirm preparation standard, cleanliness, profile where applicable, environmental conditions, mixing, application, dry-film thickness, recoat intervals and repair. For galvanizing, confirm venting and drainage provisions, surface condition, coating inspection and agreed repair procedure.
Ventura provides hot-dip galvanizing services. Project inspection should use the contract standard and approved coating procedure. Record measurement locations and instrument identification. Threads, contact surfaces, embedded items and areas requiring masking need special attention.
Handle appearance separately from protection
Runs, roughness, colour variation or distortion may have different acceptance implications from inadequate protective thickness or bare areas. Define functional and visual acceptance, especially for architecturally exposed steel. Agree repair appearance before widespread touch-up is attempted.
9. Confirm Marking and Erection Readiness
Each member should carry a durable, legible mark that matches drawings and packing lists. Orientation marks, grid references and match marks can reduce site errors. Marking must not damage the coating or appear on a prohibited exposed surface.
Review erection sequence with the packing plan. A member required first should not be trapped under later-stage steel. Confirm lifting points or handling restrictions, centre-of-gravity concerns, temporary stability needs and any site weld or field-bolt notes. The Ventura fabricated-structures range shows the breadth of possible products; dispatch controls must be tailored to the actual assembly.
10. Review Packing, Protection and Transport
Packing should prevent coating damage, water traps, abrasion, bending and loss of small components. Use suitable separators, supports and restraints. Identify bundle weight, lifting method and stacking limitations. Protect machined, threaded or prepared connection surfaces as required.
The transport plan should consider member length, width, route, permits, vehicle support points and unloading equipment. Photograph the load before departure. A dispatch note should list bundle and piece marks so receipt inspection can identify shortage or damage promptly.
11. Assemble the Manufacturing Record Book
| Document group | Typical contents |
|---|---|
| Design control | Approved drawings, revisions, RFIs and deviations |
| Materials | Certificates, traceability and consumable records |
| Fabrication | Fit-up, welding, NDT and dimensional reports |
| Coating | Material data, conditions, thickness and repairs |
| Release | Punch-list closure, packing list and dispatch note |
| Handover | Warranty, maintenance and as-built information |
The document package should be indexed, legible and linked to piece marks or inspection lots. Buyer review should occur progressively so dossier completion does not delay dispatch. Electronic filenames need stable identifiers, not only generic labels such as “final report.”
12. Close Nonconformities Before Release
Every nonconformity should describe the requirement, observed condition, affected items, disposition and approval. Repairs must be reinspected. A concession or use-as-is decision belongs to the authorized design or quality parties, not the fabrication crew. Open punch items should be visible on the release note and accepted only where contractually permitted.
Pre-Dispatch Inspection Checklist
- Approved drawings, specifications and ITP match the fabricated revision.
- Material identification and certificates reconcile with the bill of material.
- Weld inspection and required NDT reports are complete and accepted.
- Critical dimensions and interfaces have recorded actual values.
- Coating inspection and repairs meet the approved procedure.
- Member marks, loose items and connection hardware match the packing list.
- Nonconformities and punch items are closed or formally accepted.
- Packing, lifting and dispatch sequence support safe receipt and erection.
Common Quality Verification Mistakes
Common failures include inspecting only at the end, accepting unsigned reports, using superseded drawings, losing traceability after cutting, treating visual weld inspection as the only weld control, recording no actual dimensions, measuring coating without location records, packing before punch closure and allowing site teams to discover missing hardware.
The corrective approach is simple: agree evidence before work, inspect at the process stage, identify items consistently and make release conditional on record completion. Ventura also lists vetting and verification services among its services; the project should define the exact independent or supplier role required.
Use Risk-Based Sampling Without Creating Blind Spots
Not every repetitive feature needs the same inspection intensity, but sampling should be justified. Increase attention for first-off items, new procedures, complex connections, critical interfaces, repaired work and processes showing recurring defects. Reduce sampling only when the specification permits and stable evidence supports the change. The inspection plan should distinguish a representative sample from characteristics that require one-hundred-percent verification.
Sampling records should identify the population, selected items, method and result. If a sample fails, define how the inspection scope expands and how previously accepted items are reviewed. Random selection is more credible than allowing the production team to present only convenient members. Critical piece marks and foundation interfaces often warrant direct verification regardless of general sampling rules.
Coordinate Buyer, Fabricator and Third-Party Roles
The fabricator remains responsible for process control even when the buyer or a third party witnesses inspection. The buyer should provide timely approvals and qualified decisions; the third party should report against defined requirements. A witness signature does not transfer responsibility for hidden work or design. Write the authority limits into the quality plan so inspectors do not approve unauthorized design changes.
Notification periods must match the production schedule. If the buyer does not attend a properly notified witness point, the contract should state whether work may proceed. Hold points are different and require positive release. Keep inspection requests, attendance, observations and release status in one register to prevent verbal assumptions.
Verify Site Feedback Before Repeating Production
For phased deliveries, capture site receipt and erection feedback before the next batch is completed. Repeated issues such as tight holes, reversed marks, coating damage or missing loose items may indicate a systematic workshop or packing problem. Link the site observation to affected piece marks and drawings, then implement corrective action before repetition.
A short first-article or first-bay review can be particularly valuable for modular or repeated structures. Confirm fit, erection sequence, access for bolts, temporary stability and coating repair method. Update approved production documents through controlled revision; do not rely on informal instructions passed between site and workshop.
Set Clear Acceptance and Release Authority
The release workflow should name who reviews technical records, who accepts concessions and who authorizes dispatch. An inspector can record conformity but may not have authority to accept a design deviation. Separate those roles and keep approvals traceable. If release is conditional, list the exact outstanding documents or minor actions, their owner and the deadline.
Use a final release meeting for large packages to reconcile piece counts, punch closure, dossier status, transport sequence and site readiness. Distribution of the signed release to logistics, site and commercial teams prevents an uninspected or incomplete bundle from being loaded by mistake. No physical urgency should bypass a contract hold point.
Frequently Asked Questions
1. What is steel structure quality inspection?
It is the planned verification of drawings, materials, fabrication, welding, dimensions, coating, documentation and dispatch readiness against project requirements.
2. When should inspection begin?
It should begin with document and material review before fabrication, then continue through cutting, fit-up, welding, coating and final release.
3. Is final visual inspection sufficient?
No. Many critical characteristics become hidden, and material or welding evidence cannot be recreated reliably after completion.
4. What is an inspection and test plan?
An ITP lists fabrication stages, acceptance references, responsibilities, inspection extent, records, hold points and witness points.
5. How is material traceability maintained?
Heat, batch or certificate identity is transferred to cut parts using the approved marking and record system, then linked to drawings and reports.
6. What welding documents should be checked?
Project requirements may call for procedures, qualification records, welder status, consumable control, weld maps, visual reports, NDT reports and repair records.
7. Which dimensions are most critical?
Foundation and splice interfaces, hole patterns, base plates, connection geometry, member length, straightness and coordinated equipment interfaces deserve priority.
8. How is coating quality verified?
Use the approved preparation and application procedure, environmental records, visual checks, thickness measurements and documented repair inspection.
9. What is trial assembly used for?
It verifies that complex or repeated components fit together before dispatch, reducing the need for field modification.
10. Who can approve a deviation?
Only the authority defined by the contract, normally involving the responsible designer, buyer or quality representative—not unapproved shop personnel.
11. What should be in the dispatch dossier?
Include approved drawings, material and inspection records, nonconformity closure, coating reports, packing list, release note and required handover documents.
12. How can transport damage be reduced?
Use suitable supports, separators, restraints, weather protection, handling marks and a route and unloading plan matched to member geometry.
Release Steel That Is Ready to Erect, Not Merely Ready to Ship
Pre-delivery verification protects the site programme by confirming that steel, interfaces and records are complete before the load leaves the workshop. Review Ventura Salasar’s heavy steel structures, quality-focused company profile and fabrication services, then use the Ventura contact page to request a proposal with an agreed ITP, inspection records, coating controls and project-specific dispatch dossier.



Copyright © 2023-2026 Ventura Salasar | All Rights Reserved | Website Design, Developed & Google Promotion by VRD Creative Pvt Ltd